Description
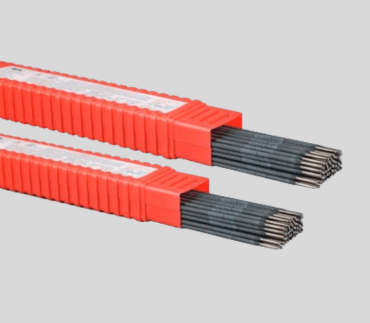
FN-55 Electrode
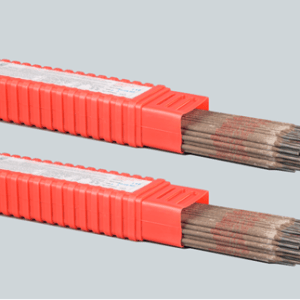
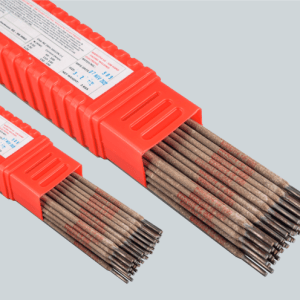
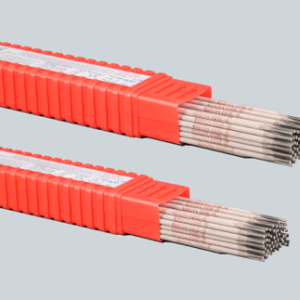
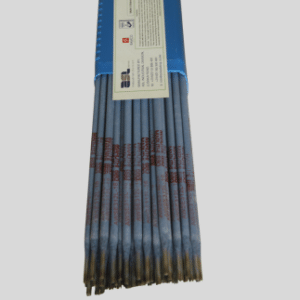
MARUTHI FN-55 is a nickel cored electrode used for the welding of all types of cast irons and particularly for the joining of austenitic alloyed cast irons; called Ni-resist. It gives a very stable arc and negligible amount of easily removable slag .Weld metal can easily be machined and has same color with that of the cast iron. It has excellent mechanical properties and it is very resistant to cracking.
Applications
MARUTHI FN-55 is used for joining and build-up welding of grey cast iron, nodular cast iron, and malleable cast iron components. It is suitable for welding parts exposed to dynamic forces, such as the bases and bodies of heavy machinery.
It is also ideal for joining cast iron components to stainless steel or other steel parts. Additionally, it can be used to fill cavities in castings or cavities that may develop after machining.
Welding Recommendations
Note: When welding cast iron without preheating, use the smallest possible electrode diameter and the lowest possible welding current to limit the width of the heat-affected zone caused by excessive heating.
When welding thick workpieces, preheating to 150–200°C followed by slow cooling is recommended.
Mechanical Properties (Weld All Metal)
| Property | Value |
|---|---|
| Yield Strength | 320 – 360 N/mm² |
| Tensile Strength | 430 – 470 N/mm² |
| Elongation (L=5d) | 10% |
| Hardness | 160 – 200 HB |
Welding Parameters AC (Min 50V) / DC (+)
| Electrode Ø (mm) | Current (Amps) |
|---|---|
| 2.50 | 45 – 80 |
| 3.20 | 60 – 120 |
| 4.00 | 90 – 140 |